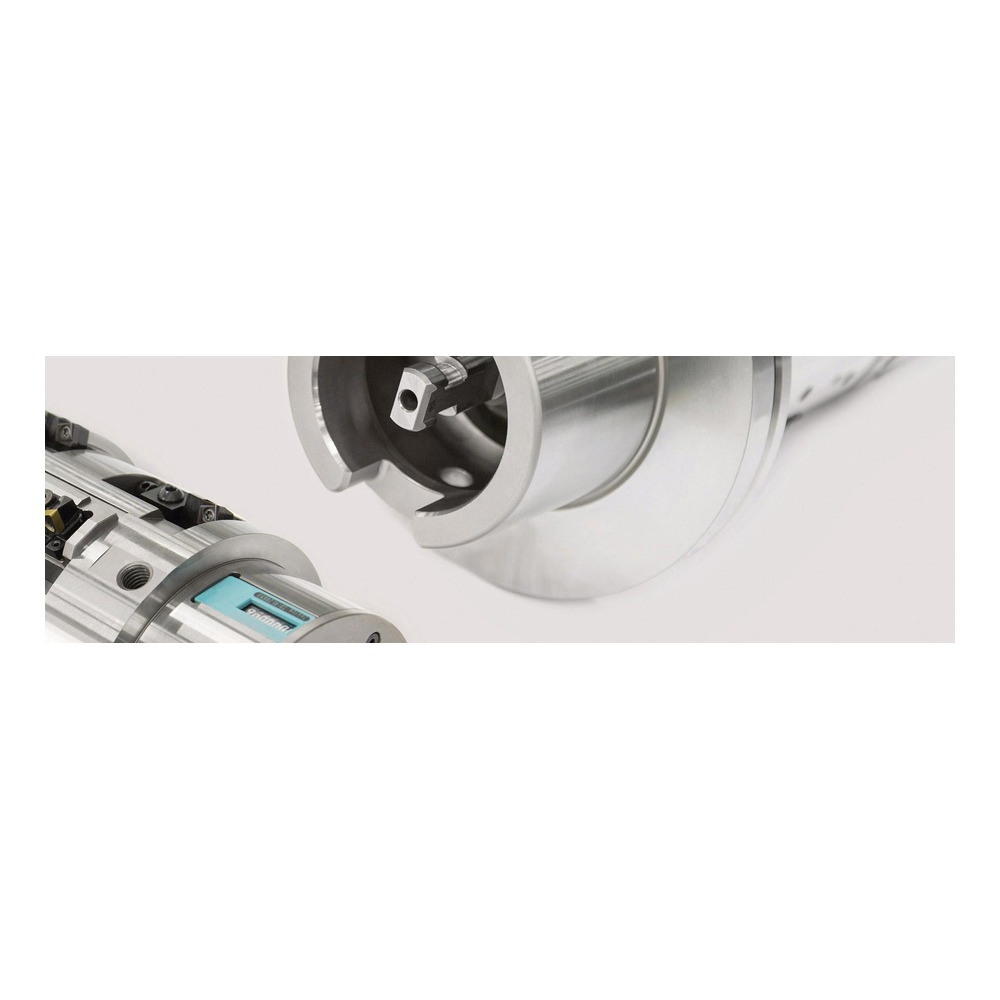
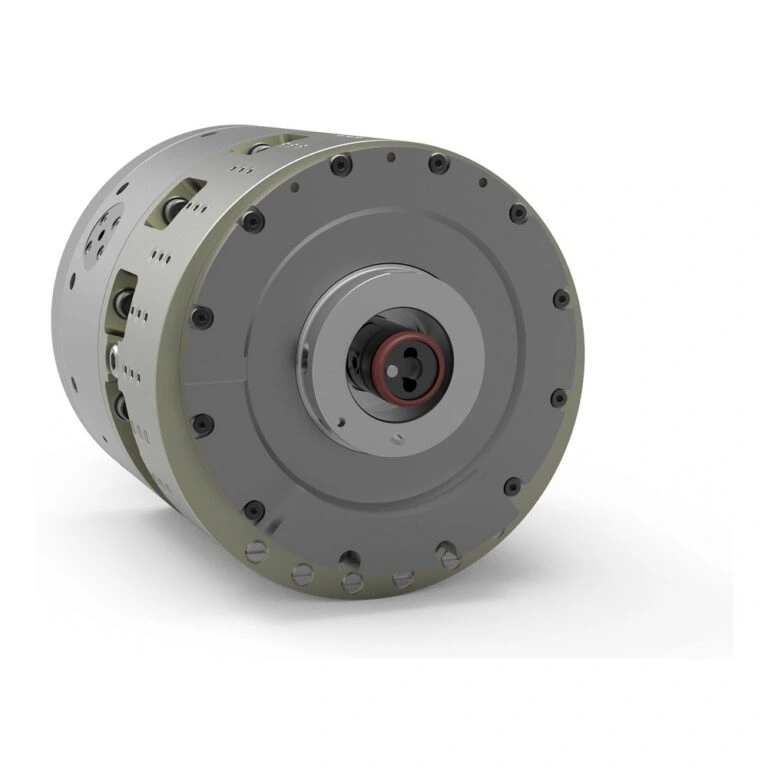
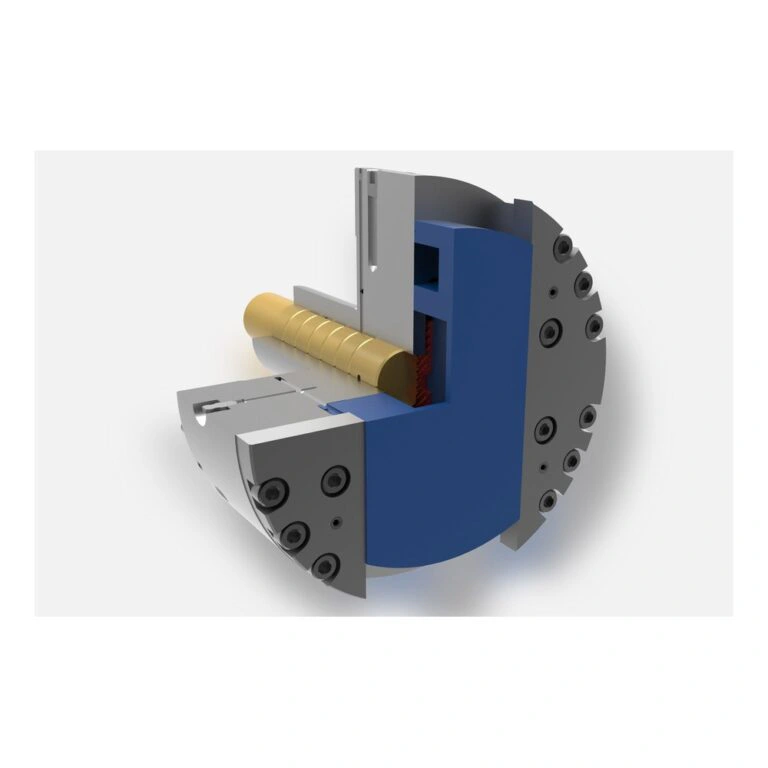
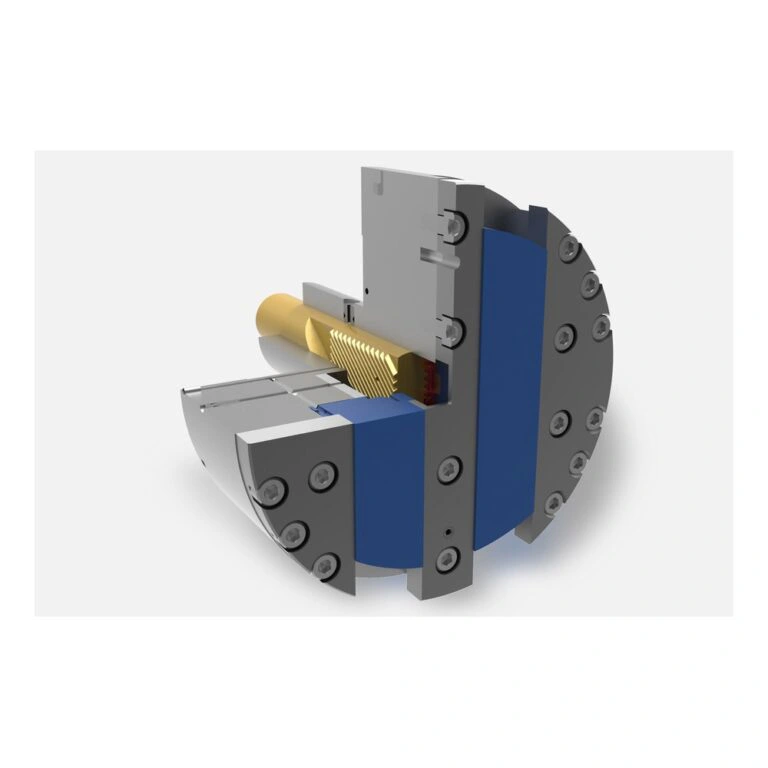
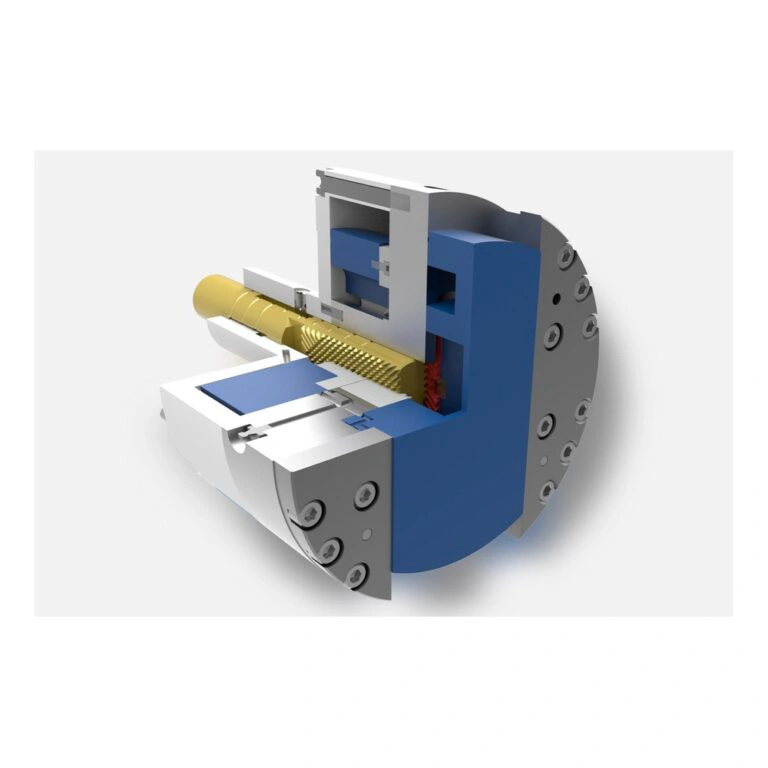
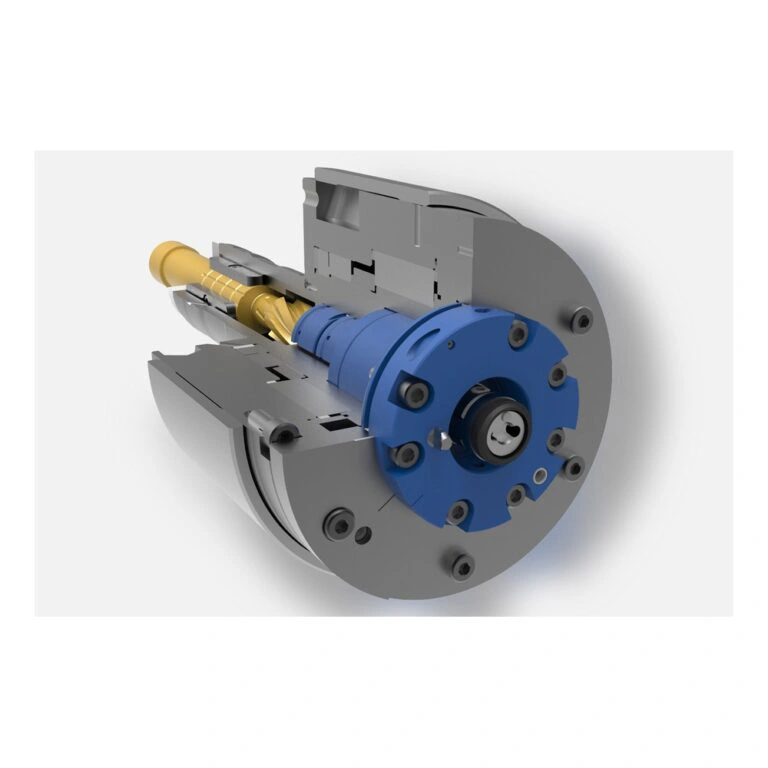
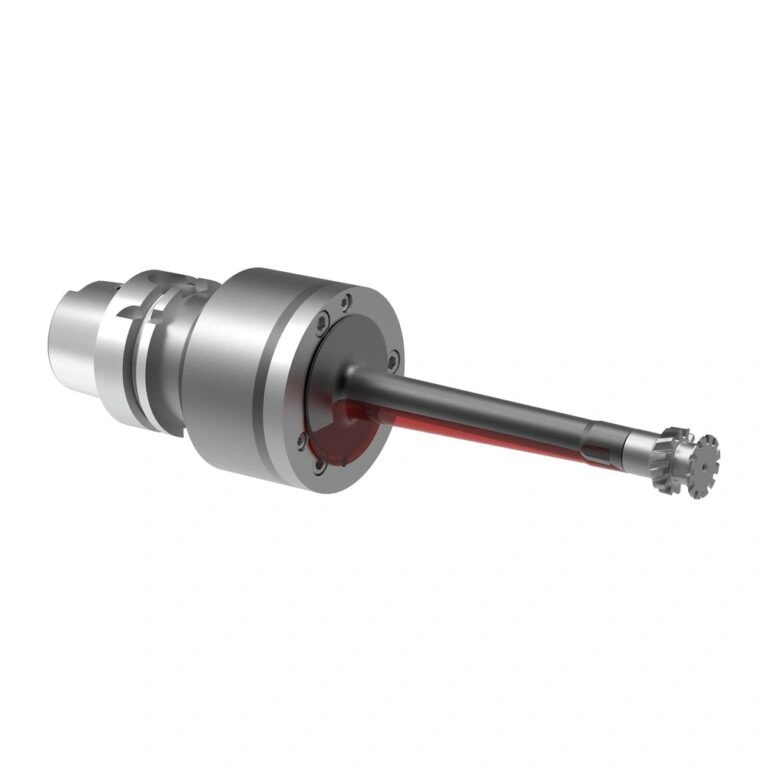
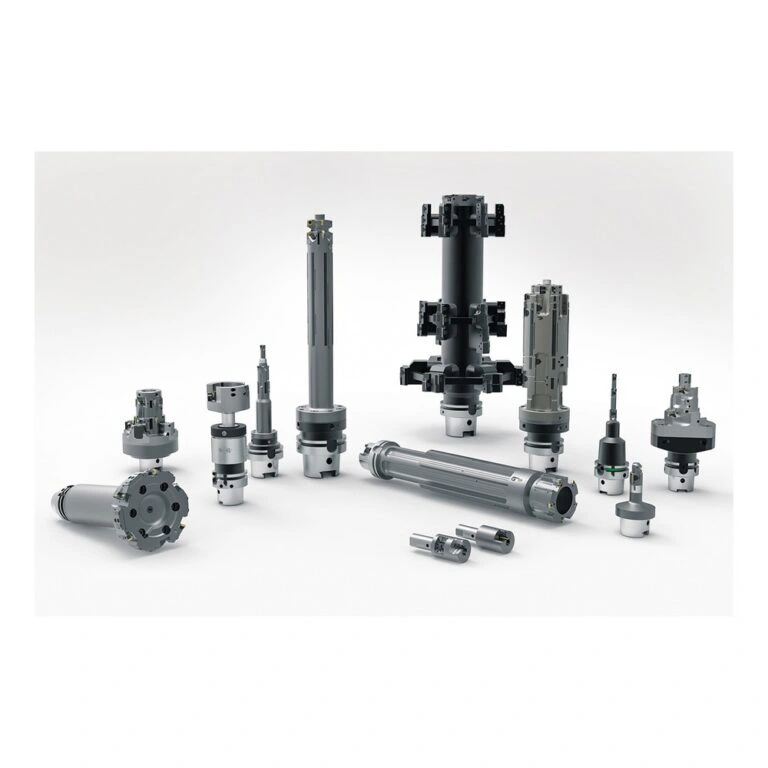
Input by means of coolant pressure The coolant pressure regulates the actuation of the slide or the positioning of the inserts. The feed rate is set manually via a regulator valve.
Key Features
- Input by means of coolant pressure The coolant pressure regulates the actuation of the slide or the positioning of the inserts.
- The feed rate is set manually via a regulator valve.
- Slides or inserts are returned via an internal spring.
- Tools actuated by coolant pressure can be used in machining centres without actuating function due to their variable connection.
- Input by means of contact stop principle With this principle the contact stop socket comes into contact with the fixture or the workpiece.
- As a consequence the tool adapter is pressed into the tool and the slide actuated.
- The feed rate is defined by the machine axis.
- The slide is retracted by an internal spring.
- Tools actuated by contact stop can be used in machining centres without actuating function due to their variable connection.
- Input by means of TOOLTRONIC U axis / U axis spindle integration As a self-contained drive module, TOOLTRONIC represents a fully-fledged NC axis integrated into the machine control system that makes possible a wide range of applications using inductive energy and bidirectional data transmission.
Technical and Application Information
Input by means of coolant pressure The coolant pressure regulates the actuation of the slide or the positioning of the inserts. The feed rate is set manually via a regulator valve. Slides or inserts are returned via an internal spring. Tools actuated by coolant pressure can be used in machining centres without actuating function due to their variable connection.
Input by means of contact stop principle With this principle the contact stop socket comes into contact with the fixture or the workpiece. As a consequence the tool adapter is pressed into the tool and the slide actuated. The feed rate is defined by the machine axis. The slide is retracted by an internal spring. Tools actuated by contact stop can be used in machining centres without actuating function due to their variable connection.
Input by means of TOOLTRONIC U axis / U axis spindle integration As a self-contained drive module, TOOLTRONIC represents a fully-fledged NC axis integrated into the machine control system that makes possible a wide range of applications using inductive energy and bidirectional data transmission. The slide is actuated by an actuating motor in the tool. As a general rule, actuating tools that were activated in the past by coolant pressure, the contact stop principle or using a drawbar, can be driven and controlled both on machining centres and special machines without actuating function with TOOLTRONIC.
Input by means of the machine's U axis The slide is actuated via the U axis on the machine tool. The feed rate is set via the U axis. As a rule this axis is rotary and a fully functional NC axis. Wherever machining centres are equipped with U axis systems, suitably prepared controllable tools can be used.
Input by means of drawbar/push rod In a special machine, the central drawbar/push rod can be used for actuating the slide or positioning the inserts. The feed rate is set via the U axis. This axis also provides the retraction (NC-controlled).
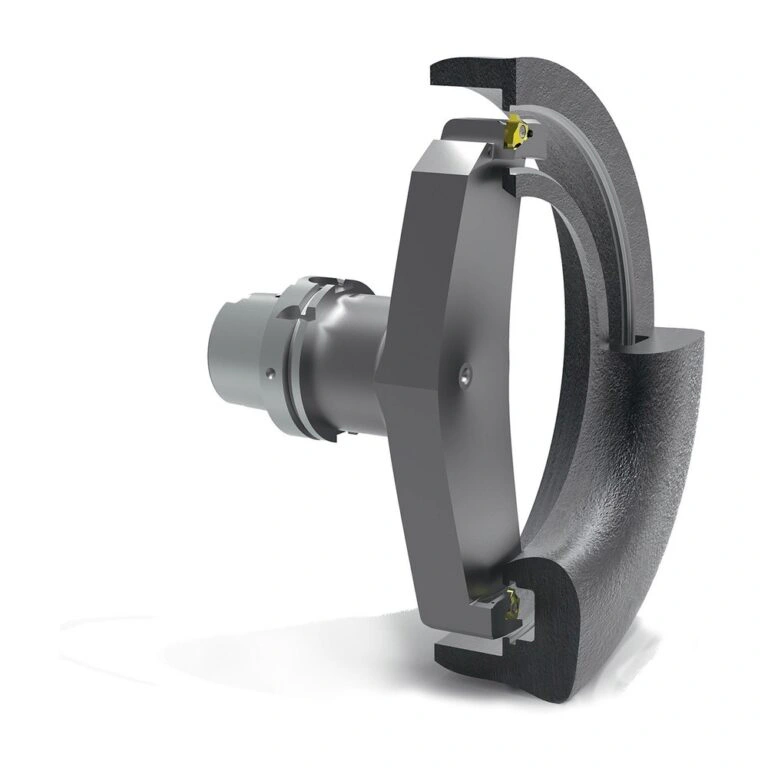
Linear slide The linear slide, which is perpendicular to the centre line of the tool, is actuated via angled teeth on the drawbar/push rod. Machining operations: Recessing Contour turning Facing Thrust bearing turning
Inclined slide The inclined slide's angle in relation to the centre line of the tool that is not 90°. It is actuated via angled teeth on the drawbar/push rod. Typical machining operations: Recessing Chamfering Taper turning
Pivoting slide The pivoting slide is operated via a central pin using an internal lever mechanism. A spherical segment is produced by the inherent rotation of the tool and the superimposed rotation of the pivoting slide. Machining operations: Turning spherical ball
Rotary slide The rotary slide is actuated via a combination of twist shaft and twist sleeve. During this process the axial movement of the twist shaft is converted into a rotation using a twist sleeve. The radial stroke is provided by an eccentric located slide. Typical machining operations: Recessing Contour turning Facing Thrust bearing turning
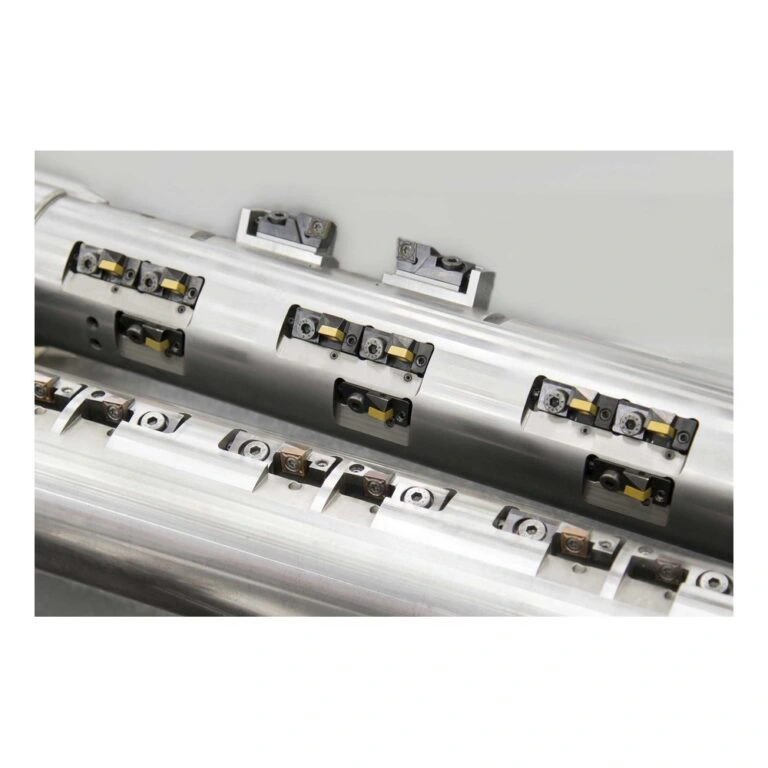
Deflection and tilting holders An angled surface on the drawbar/push rod is responsible for the actuation of the cartridge on the deflection holder and the tilting holder. The holder is set to the appropriate centrifugal circle diameter depending on the position of the drawbar/push rod. Typical machining operations: Compensating cutting edge wear Turning small contours Recessing